Extrusion Pullers
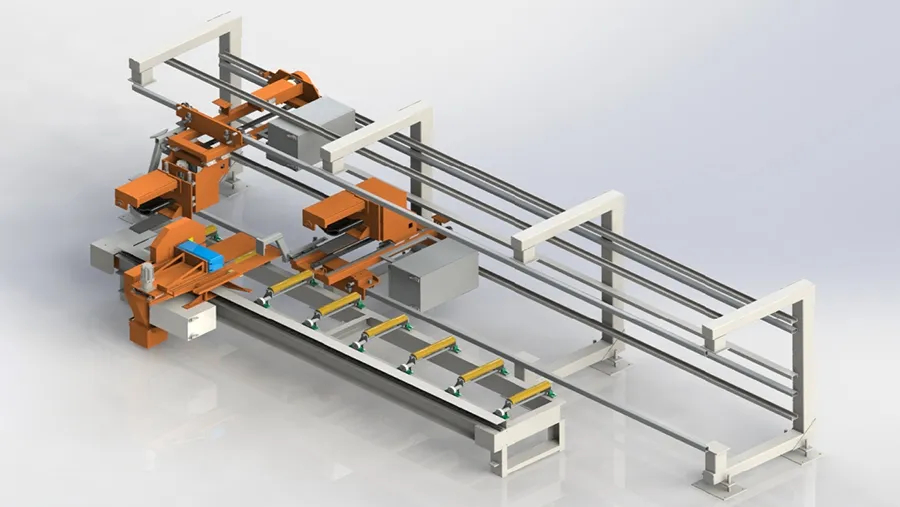
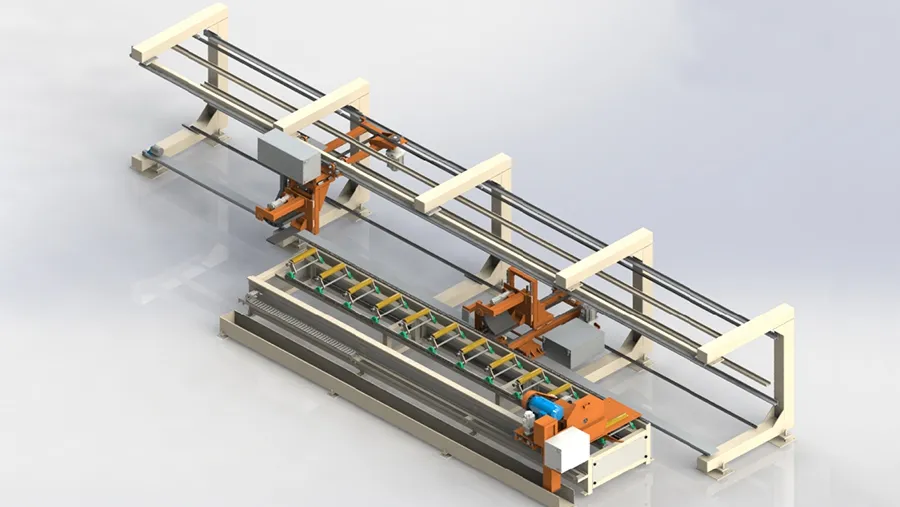
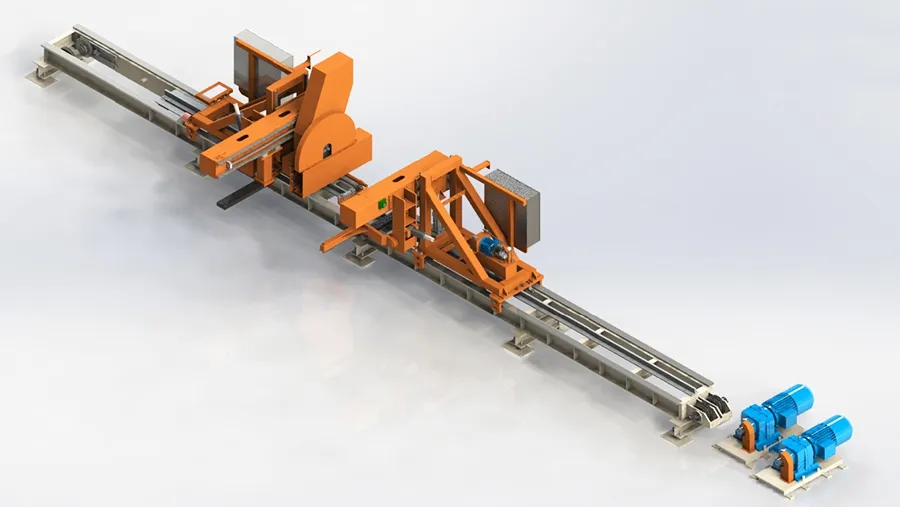
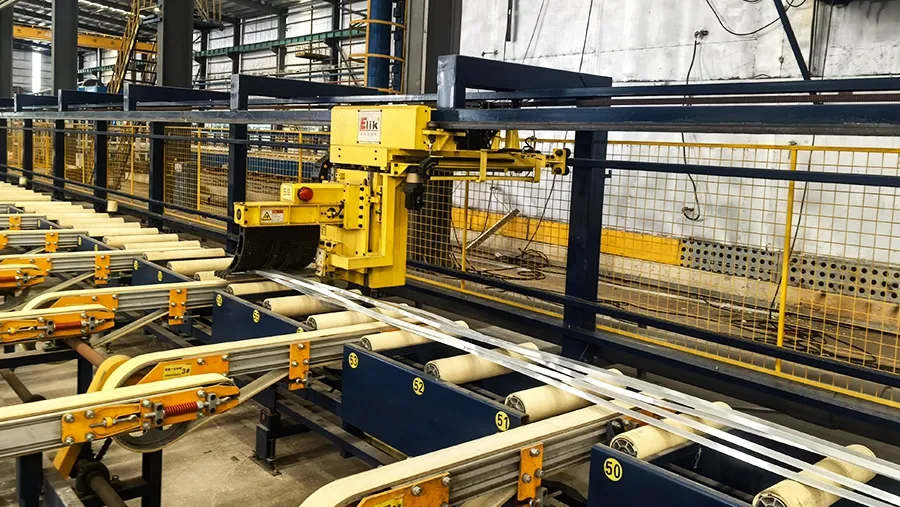
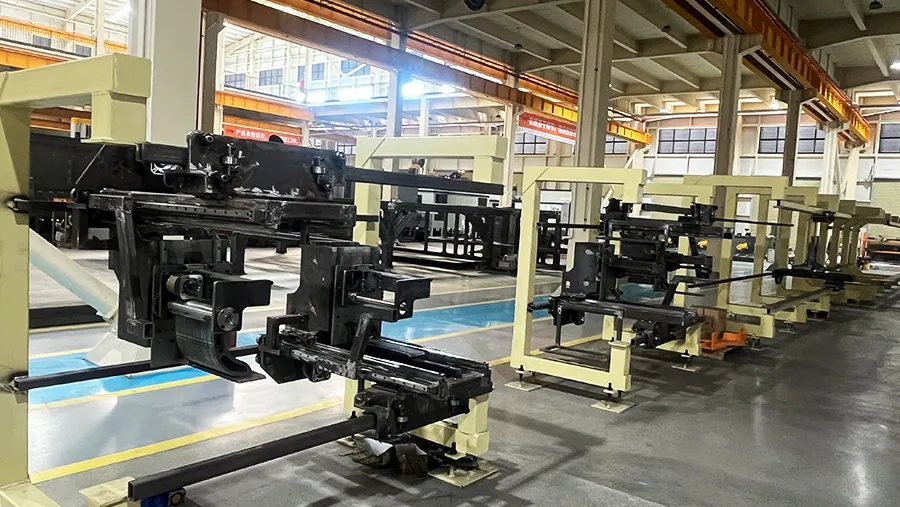
The puller is situated immediately at the press (in-line quench) outfeed and is capable of performing three tasks simultaneously: synchronized grasping, constant-tension straightening, and cut-to-length conveying. The freshly extruded profile, which is still soft at 500–580°C, is drawn out of the press at a steady speed, straight, and under minor tension. This prevents bending, twisting, stacking, and scratching. In doing so, it directly influences the profile's straightness, surface quality, and material yield.
ELIK provides a twin-head dual-track puller and an articulated (hinged) dual puller.
The articulated dual puller employs two symmetrically arranged pulling heads that are typically powered by pneumatic or hydraulic cylinders to facilitate rapid clamping. It is well-suited to small-to-medium production lines and installations where floor space is constrained due to its more restricted adjustment range.
One synchronized automatic cut-off saw is integrated with two drawing heads (P1, P2) in the twin-head dual-track puller. In comparison to a two-head dual-track puller, it streamlines the production sequence, reduces the work cycle, and employs a lighter, simpler frame. The return speed is significantly reduced as a result of the two identical heads pulling alternately, which reduces equipment wear and simplifies maintenance. This design significantly increases both throughput and yield by addressing the demands of multi-hole dies, multiple cuts per log, easily deformed thin sections, and high-speed extrusion of complex profiles.
| Parameter | Value |
| Compatible press | 600–7500T |
| Pulling speed | 1–80m/min (variable-frequency adjustable) |
| Pulling force | 10–1500kg (constant-tension adjustable) |
| Jaw opening | 0–500mm (matched to profile height) |
| Control | PLC + servo closed-loop synchronization |
- Servo constant tension provides superior surface quality, a higher yield, and high cross-sectional dimensional accuracy due to low tension fluctuation.
- Intelligent synchronization is a central control system that facilitates the one-touch coordination of the press, puller, in-line quench, intelligent cooling table, and finished-product saw. Keeping upstream and downstream material flow securely in sync, full-line operating data is dynamically aligned and shared in real time. Fast format changes are implemented.
- Arc self-locking segmented jaws are equipped with a hard, anti-slip wear-resistant alloy layer or a high-temperature protective material on the gripper faces. They automatically adjust to intricate hollow or irregular industrial sections, prevent slippage, and maintain a secure grip while avoiding the compression or twist-scratching that thin-wall material is susceptible to.
- Frame & track
Heavy steel frame with single or multiple tracks; the track is precision-leveled for solid, judder-free head travel. - Pulling head (jaw + drive)
Arc self-locking segmented jaws adjust automatically to uneven sections, preventing hollow thin-wall material from twisting. A servo or gearmotor combined with a chain or rack-and-pinion drive provides consistent torque and tension control. A power-loss brake stops a runaway. - Transmission
Rack-and-pinion or chain. - Control (PLC + servo)
Real-time closed-loop synchronization with the press; constant-tension control that automatically matches pulling speed; and encoder length measuring for precise cut-to-length. - Safety & auxiliary
Emergency stop, anti-collision, and high-temperature protection; automatic lubrication, fault detection, and remote monitoring.