Cooling Table
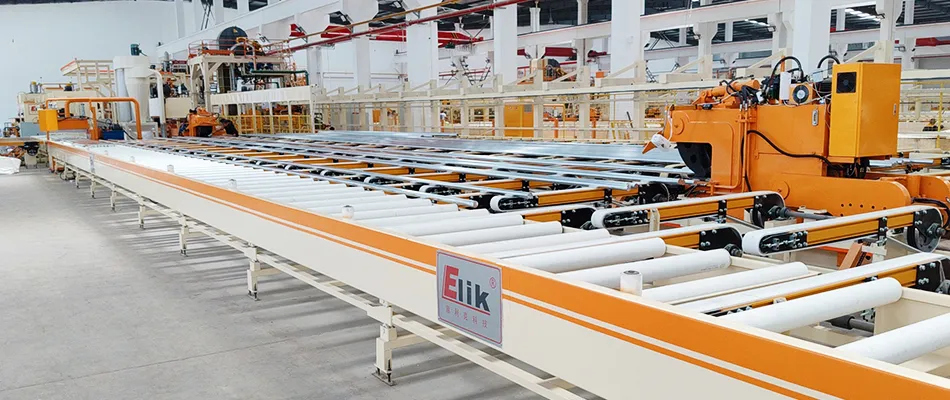
The aluminum extrusion line's primary rear-end system is the cooling table. Placed immediately following the press, it receives the profile that has just been formed, which is extremely hot. It then manages the transitional preparation before stretch-straightening, as well as high-efficiency cooling and seamless conveying. This process safeguards the profile's physical properties and surface quality. In practice, ELIK's cooling table functions as a comprehensive run-out handling line, transporting the profile from die exit to straightening, cooling, and cut-to-length sawing.
Overall: 32m × 8m, 1.23m pitch; 4-level conveying.
| Item | Parameter |
| Press tonnage/billet diameter | 1450T / Φ152mm |
| Cooling table placement | Front-end sawing |
| Cooling table length | 32,000mm |
| Cooling table width | 8,000mm |
| Slide-out table length | 13,000mm |
| Max. profile size | W: 240mm × H: 150mm |
| Max. profile weight per metre | 8kg/m |
| Voltage/frequency | 380V / 50Hz |
| Ref | Mechanism | Model / specification | Qty |
| A | Initial run-out table | Height-adjustable | |
| Overall dimensions | 13,000 × 500mm (of which the puller's automatic in-line cut-off saw occupies 4.5m) | ||
| Cooling fans | Upper: 7 × 0.75kW axial fans with 6m air trough; Lower: 7 × 0.55kW axial fans | ||
| B | Slide-out table | Hydraulic lifting type | |
| Overall dimensions | L: 32,000 × W: 500 × raised height H: 820mm | ||
| High-temp felt rollers | Φ76 × 10 × 400mm, rated 480°C, 410mm pitch | 1 set | |
| Hydraulic station | 2.2kW motor | 1 set | |
| Cylinder | Φ63 × 250mm | 1 set | |
| C | Pick-off table (Level 1) | Automatic feed | |
| Overall dimensions | L: 32,000 × W: 1,000 × H: 800mm (actual dimensions govern) | ||
| Feed mechanism | Aluminum-beam felt belts, horizontal transverse feed | 26 strips | |
| High-temp felt belts | 80mm wide × 10mm thick, rated 480°C | 26 strips | |
| Felt-belt aluminum beams | Aluminum guide channel 100 × 90, incl. sprocket and adjustment fork plate | 26 strips | |
| Cycloidal-pin gear reducer | 2.2kW | 1 unit | |
| Drive shaft | Φ40mm round steel | 1 set | |
| D | Cooling table (Level 2) | ||
| Overall dimensions | L: 32,000 × W: 2,000 × H: 810mm (actual dimensions govern) | ||
| Feed mechanism | Aluminum-beam felt belts, horizontal transverse feed | 27 strips | |
| High-temp felt | 80mm wide × 10mm thick, rated 480°C | 27 strips |
- Die exit → slide-out table: the profile departs at approximately 520°C and is drawn out by the puller onto the slide-out table. Felt rollers protect against scratching and cushion the impact.
- Transition roller table → onto the cooling table: the profile transfers smoothly; a pull-across mechanism separates profiles into single lengths at an adjustable 50–300mm spacing.
- Zoned forced-air cooling (core cooling section): approximately 20–30 meters in length and divided into 3–5 air zones: the front zone, which has a high air volume and rapid cooling to approximately 300°C; the middle zone, which has a medium air volume and uniform cooling; and the rear zone, which has a low air volume and fine trim to a stable discharge of ≤150°C.
- Discharge → straightener/saw: the profile is sufficiently rigid and internal tension is relieved once the temperature is reached.
- Automatic feed to the stretch-straightener (removing minor bends) or cut-to-length saw.
- Scrap/off-cut handling: tail ends are automatically sorted and returned to remelt, ensuring that there is no manual contact with the hot profile. This process is both safe and efficient.
Slide-out (hot run-out table)
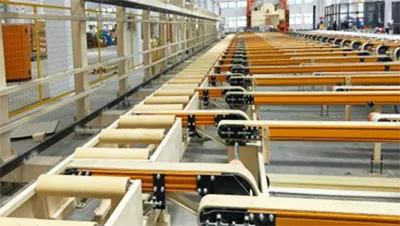
Composed of a square-tube base frame and a set of high-temperature felt rollers, the table is welded from A3 folded steel plate. A single hydraulic cylinder drives a wedge-plate device that elevates and lowers the entire table.
Level 1: Pick-off table
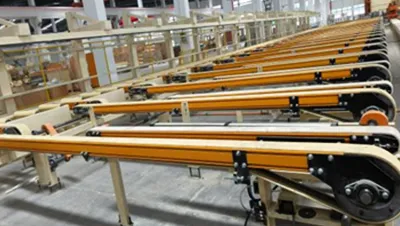
The slide-out table descends to transfer the profile onto the pick-off conveyor belt when the profile is prepared for transverse transfer. The belt subsequently moves the profile laterally onto the cooling table, and the slide-out table rises to complete one cycle. Felt belts are easily replaceable and can be replaced independently.
Level 2: Cooling table
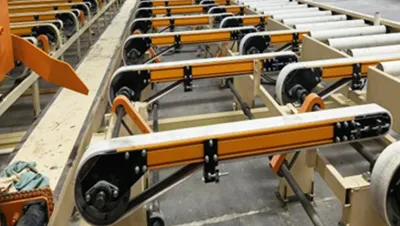
The profile is ready for transfer to the straightener. The base frame is square-tube; the belt-support beams are aluminum with deep guide channels for belt tracking; and the felt can be replaced independently for ease of adjustment and maintenance.
Level 3: Straightening
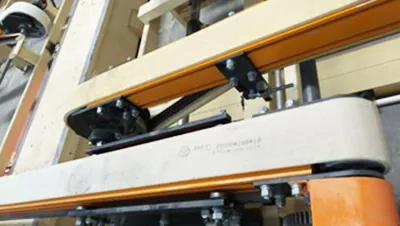
Transfer table
The straightener's transition belt-conveyor system, which employs translatable aluminum-beam belts with a geared drive to ensure more precise belt travel.
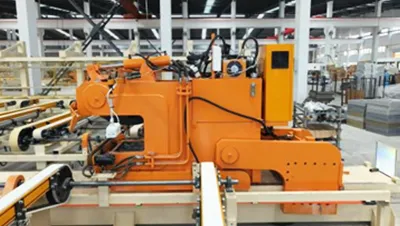
Straightener
A hydraulic stretch-straightener with a reverse-thrust main cylinder, characterized by a high stretching force, stable operation, and a rapid idle-stroke speed. The profile's release height is consistently established by the down-press jaw, which prevents damage or distortion during the release process. This improves idle-stroke efficiency and reduces straightening distortion.
Level 4: Storage table
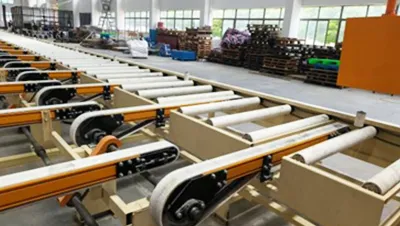
Similar in structure to the cooling table and is also belt-conveyed. It carefully arranges straightened profiles and feeds them to the finish-saw roller table.
Table for sawing and cutting to length
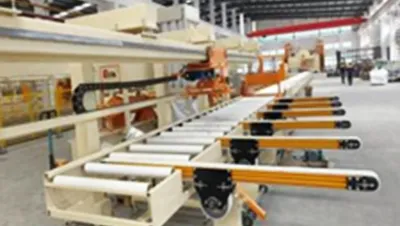
Roller table
A powered roller conveying device that has the same structure as a slide-out table.
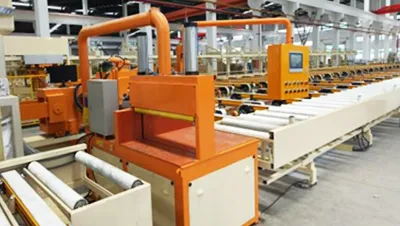
Finish saw
Taiwan high-precision linear guides for a more durable and smoother saw feed; clean, flat cuts; safe operation; and quick, simple maintenance. A pressure-regulating valve is utilized to clamp material in a pneumatic cylinder. The finish saw is equipped with a cyclone aluminum-chip recovery unit and a spray-lubrication unit, featuring a recovery rate of up to 90%.
- Controlled air volume and speed to facilitate gradual cooling, thereby preventing the distortion or cracking that results from rapid chilling.
- Uniform cooling and distortion prevention: the profile is uniformly supported along its entire length without any sagging. The cross-sectional temperature difference is maintained at ≤10°C by the top-and-bottom air-blast, which minimizes waviness, twisting, and bending. The profiles are separated into single lengths without any mutual contact, ensuring that each one receives an even amount of ventilation.
- The press and puller are connected to the PLC for automatic control. The fan frequency, travel speed, and automatic cut-to-length sawing are adjusted to the profile's section and length. The straightening tension is auto-regulated, allowing for single-operator or unattended straightening.
- High-temperature wear-resistant felt rollers: long service life, no aluminum pick-up, no scattering.
- Comprehensive safety features include infrared anti-pinch, emergency stop, and high-temperature-zone isolation.