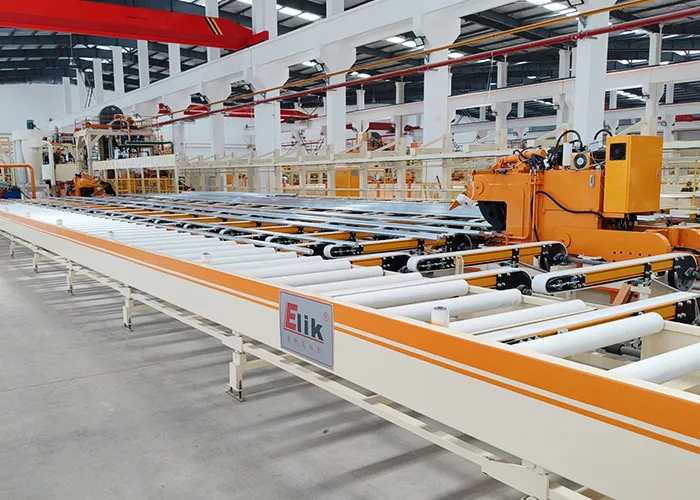
A profile's final quality is still being determined the moment it exits the die. The material's temper, straightness, and surface finish are determined by how it is cooled, pulled, and handled in the seconds and minutes after extrusion. ELIK provides the three in-line units that regulate this critical run-out stage.
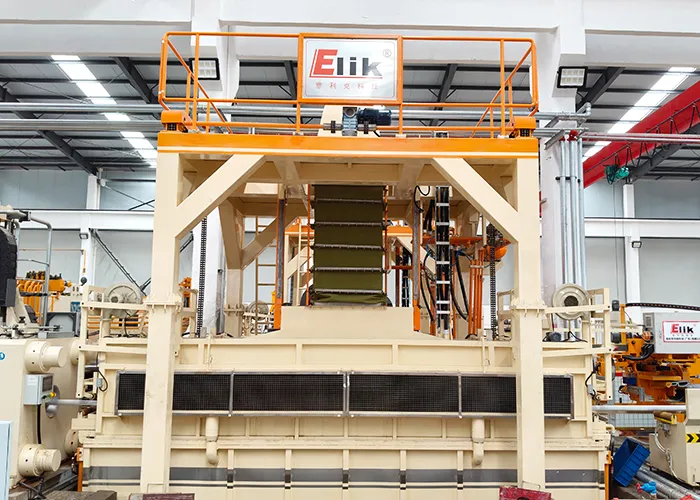
- In-line quench system
Hot profiles are quenched immediately upon exiting the die. The system is capable of matching the quench rate to the alloy, thereby achieving the appropriate mechanical properties for materials of varying strengths, through the use of three cooling modes: air, water, and water-mist. - Puller
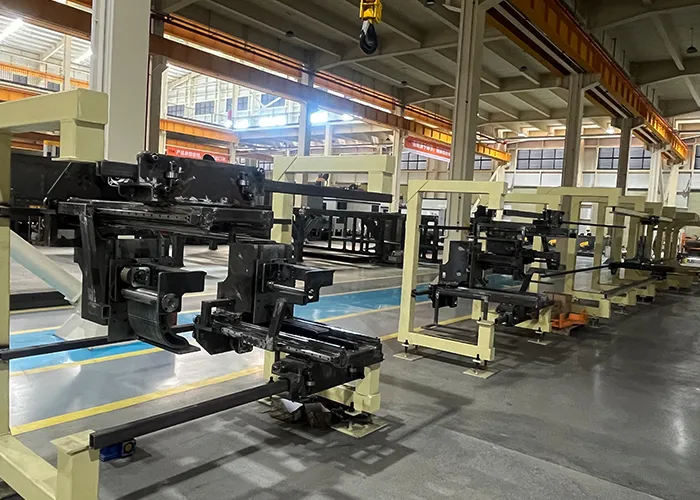
The puller operates in tandem with the extrusion speed, drawing the profile under constant tension to prevent micro-scratches and cross-sectional distortion as the profile develops. - Cooling table
The extruded profiles are effortlessly transferred onto the cooling table for controlled natural cooling and pre-straightening rest. The entire extrusion line is maintained in a continuous and stable state by the integrated automatic transfer and layered stacking, which arrange profiles in order, prevent surface scratching and warping, and feed the downstream straightening, sawing, and inspection stages.
The profile's properties and surface are safeguarded during the most vulnerable stage of production by these devices, which serve as a connection between the press and the finishing line.
Elik is a company specializing in the R&D and manufacturing of aluminum extrusion processing equipment and industrial furnaces. It provides aluminum profile processors with equipment for ingot pre-treatment, inline post-extrusion handling, and offline heat treatment. Elik possesses the capability to design and deliver fully integrated production lines, with an annual production capacity of 300 energy-efficient heating furnace units and 20 complete production lines.